
20.4Material requirements#
20.4.1Steel components#
Steel components shall be manufactured to the details shown on Standard Drawings 1467, 1470, 1474, 1475, 1476, 1477, 1478, 1479, 1480, 1481 and 1482.
All steel components shall be hot-dipped galvanised after manufacture in accordance with the requirements of AS/NZS 4680.
20.4.2Panels#
20.4.2.1Material requirements#
Steel beam guardrail panels shall be manufactured to the detail shown on Standard Drawings 1480 and 1481 from steel conforming to the requirements of AS/NZS 1594 grade HA350.
When tested in accordance with AS 1391, the mechanical properties of the base metal shall conform to the requirements of Table 20.4.2.1(a).
| Property | Limits |
|---|---|
| Yield Stress, Minimum | 340 MPa |
| Ultimate Tensile Stress, Minimum | 450 MPa |
| Elongation, Minimum | 15% |
The panel section after rolling shall have a maximum tolerance on camber in any 2,500 mm length of 4.5 mm.
The base metal strip used for fabrication of guardrail panels shall conform to the tolerances listed in Table 20.4.2.1 (b).
| Property | Tolerance (mm) |
|---|---|
| Base metal thickness (2.7 mm) | + 0.21 |
| Mill tolerance on strip width | + 2.5 – 0 |
Terminal sections and stiffener plates shall be fabricated from similar material to guardrail panels.
20.4.2.2Batch marking requirements#
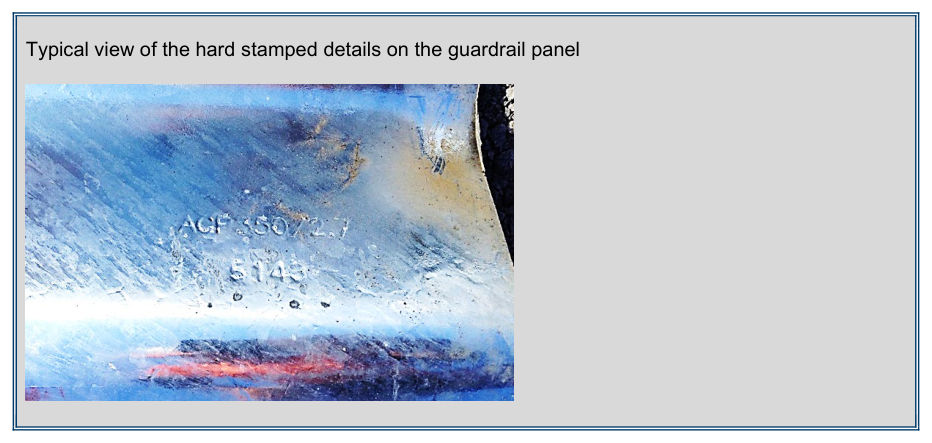
All panels shall be hard stamped during the manufacturing process with the following information:
- a)Manufacturer’s unique company identification.
- b)Grade of material and base metal thickness, and
- c)Unique batch number of product which is produced from:
- i.a single coil of steel
- ii.identifiable multiple coils of steel used in the manufacture process.
A single batch shall consist of no more than 2000 items.
Materials test certificates shall comply with the requirements of Clause 20.4.5.
20.4.3Steel posts and blockouts#
20.4.3.1Material requirements#
Steel posts and blockouts shall be fabricated from steel conforming to the requirements of AS/NZS 1594 grade HA300.
20.4.3.2Batch marking requirements#
All steel posts and blockouts shall be hard stamped during the manufacturing process with the following information:
- a)Manufacturer’s unique company identification.
- b)Grade of material and base metal thickness, and
- c)Unique batch number of product which is produced from:
- i.a single coil of steel
- ii.identifiable multiple coils of steel used in the manufacture process.
A single batch shall consist of no more than 2000 items.
Materials test certificates shall comply with the requirements of Clause 20.4.5.
20.4.4Steel plate, strip, bar and attachments#
Steel plate, strip, bar and attachments shall conform to the requirements specified on the Standard Drawings elsewhere mentioned in Clause 22.
Materials test certificates comply with the requirements of Clause 20.4.5.
20.4.5Material conformance#
All the steel manufacturer material test certificates shall be supplied to the Administrator. The steel manufacturer’s test certificates shall show the following:
- a)full chemical composition including the carbon equivalence, and
- b)mechanical test results for yield, tensile and elongation.
The Administrator shall review and approve the material test certificates. Hold Point 7
If test certificates are not available, then the Contractor shall submit to the Administrator for approval a proposal for selecting samples for testing of mechanical properties and chemical analysis and in accordance with the appropriate Australian Standard at no expense to the Principal. Witness Point 2 Minimum testing requirements are four samples of each production batch.
20.4.6Material audit testing#
All guardrail posts and panels shall be audit tested by the Administrator using one of the following options.
20.4.6.1Project testing#
All projects shall be supplied with a minimum of two extra posts and two extra panels from each batch of panels and posts supplied to the project.
The Administrator shall randomly select two post and two panels from each batch number for audit testing. Witness Point 3
20.4.6.2Previous project testing#
Posts and panels which have previously been project tested can apply to the Administrator for a concession on carrying out the project testing, provided the batch marking numbers match the audit test reports.
20.4.6.3Testing requirements#
The posts and panels shall have the following tests undertaken:
- a)dimensional check with departmental Standard Drawings
- b)full chemical composition including the carbon equivalence
- c)determine the Base Metal Thickness (BMT), and
- d)mechanical test results for yield, tensile and elongation.
Installation shall not commence until the Administrator has confirmed the materials tested match the material test certificates supplied for the batch of guardrail components. Hold Point 8
Guardrail components which do not match the product supplied shall be rejected and replaced with new guardrail components with a different batch number.
20.4.7Fasteners#
Hexagonal head bolts and nuts shall be manufactured to the dimensions shown on the Standard Drawings noted in Clause 20.4.1. These fasteners shall comply with the requirements of AS 1111.1, AS 1112.3, AS/NZS 1252 as appropriate. These fasteners shall be tested in accordance with the requirements of MRTS78 Fabrication of Structural Steelwork.
Mushroom head bolts, product Grade C, shall be manufactured to the details shown on Standard Drawing 1479 and shall comply with AS/NZS 1390. Mushroom head bolt assemblies designated as Class 4.6 shall have the chemical and mechanical properties outlined in AS 1111.1 and AS/NZS 1112.3. Mushroom head bolt assemblies designated as Class 8.8 shall have the chemical and mechanical properties outlined in AS/NZS 1252. These fasteners shall be tested in accordance with the requirements of MRTS78 Fabrication of Structural Steelwork.
Where the length of the bolt, in accordance with AS/NZS 1252, both hexagonal and mushroom head, prevents it from being mechanically tested no assembly test will be required.
Circular washers to conform to AS 1237.1 and taper washers to conform to AS/NZS 1252.
All fasteners to be hot dip galvanised to AS/NZS 1214.
20.4.8Delineators#
Delineators shall comply with the requirements specified in Clause 10.2.4 and in accordance with the requirements of Standard Drawing 1478.
20.4.9Cable and Cable assembly#
Cable shall be right ordinary lay rope (sZ) conforming to AS 3569 and as detailed on Standard Drawing 1479. Cable assembly (FC01) shall be in accordance with Standard Drawing 1479. A NATA certified test certificate outlining the mechanical test results for breaking strength (must withstand 200kN minimum), of the cable assembly shall be included in the quality records.
The test certificate shall be traced back to the individual cable assemblies supplied to the project, via an identification tag.